
Reliability Starts With Context
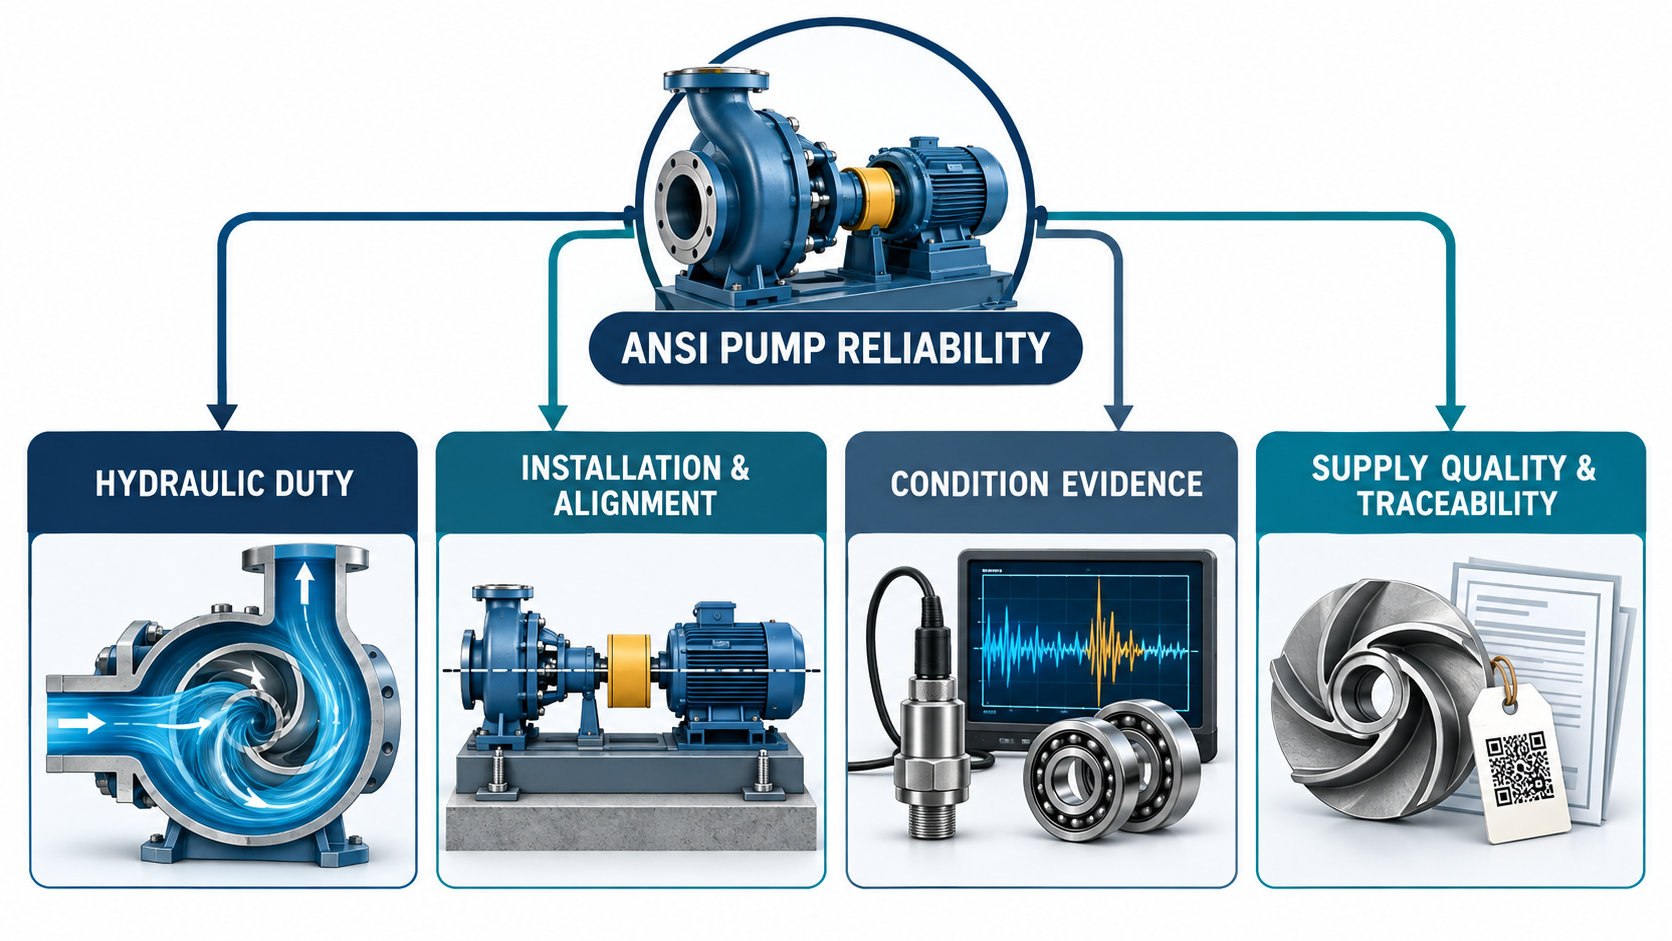
A component failure is evidence, not a complete diagnosis. Repeated seal leakage, bearing damage or vibration should be connected to the pump’s hydraulic duty, installation, condition trend and replacement-supply evidence before the same repair is repeated.
The purpose of the four-pillar framework is to determine what evidence should be checked before repeating the same repair.
Start With the Symptom — Then Collect Evidence
Field symptoms are useful starting points, but they should narrow the investigation rather than define the root cause.
| Field symptom | First evidence to collect | Check first | Do not assume |
|---|---|---|---|
| Repeated mechanical-seal leakage | Duty, suction condition, seal arrangement, alignment and runout evidence | Hydraulic + Installation | The seal itself is automatically the root cause |
| Repeated bearing failure | Vibration, lubrication, contamination, alignment, operating point and history | Condition + Installation | Installing another bearing solves the problem |
| Cavitation-like noise or pitting | Flow, suction pressure, temperature, NPSH basis and suction losses | Hydraulic | Changing material alone corrects the hydraulic cause |
| Vibration after piping work | Alignment before/after, soft foot, flange fit and pipe supports | Installation | Rotor unbalance is automatically responsible |
| Rising bearing temperature | Trend, ambient, load, lubrication, vibration and duty | Condition | One temperature limit applies to every pump |
| Reduced flow or head | Speed, pressure, control state and pump/system curve | Hydraulic | The pump is automatically undersized |
| Replacement fits but performs poorly | Curve, speed, configuration, material and interfaces | Hydraulic + Supply | Dimensional fit proves complete interchangeability |
Pillar 1: Hydraulic Duty
The installed operating point is established by the interaction between the pump and the system. Design duty, original catalog duty and current field duty should not be assumed to be identical.
Confirm the Actual Duty
- Normal, minimum and maximum flow.
- Suction and discharge pressure, developed head and actual speed.
- Liquid temperature, density, viscosity, vapor-pressure basis, solids or entrained gas where relevant.
- Valve, bypass, parallel-pump and VFD operating state.
Compare BEP, POR and AOR Correctly
Compare actual operation with the applicable pump curve and the manufacturer- or project-defined preferred and allowable operating regions. Do not turn one generic percentage around BEP into a universal acceptance rule.
Review NPSH Margin
Confirm NPSHa against the manufacturer’s NPSHr and the margin required for the actual application. Lowest liquid level, highest credible temperature, suction losses and maximum flow can all change the available margin.
Review the Control System
Throttling, bypass operation, VFD speed changes, parallel sequencing and minimum-flow logic can move the operating point even when the pump itself has not changed.
Related guide: Pump System Fundamentals: Curves, Operating Point & NPSH.
Pillar 2: Installation and Alignment
Hydraulically suitable equipment can still fail when the installed machine is loaded by its base, coupling or piping.
Check the Mechanical Installation
Review foundation, grout, anchors, baseplate condition, soft foot, coupling installation, lubrication, mechanical looseness and rotation before assigning a recurring problem to an internal pump component.
Check Alignment After Piping Connection
If attaching or tightening the piping materially changes machine position or alignment, investigate the piping and support condition rather than forcing the pump into position.
ITT Goulds 3196 i-FRAME documentation provides an operating-temperature alignment example around 0.05 mm / 0.002 in TIR. This is an OEM/model-specific example, not a universal tolerance for every ANSI B73.1 pump.
Pipe Strain Evidence
Use the applicable project, OEM or nozzle-load procedure. Do not invent one universal dial-indicator displacement limit for every installation.
Experiencing Repeat Seal, Bearing or Vibration Problems?
Send the pump model, normal operating duty and the failure pattern. Alignment records, vibration trends, photos or drawings can be added if available.
Pillar 3: Condition Evidence
Condition monitoring becomes useful when measurements are repeatable and tied to operating state. A single vibration number or temperature reading is less informative than a stable baseline and a documented trend.
| Evidence | Record | Why it matters |
|---|---|---|
| Vibration | Location, direction, overall value, spectrum/phase where available, speed and duty | Mechanical and hydraulic response |
| Bearing temperature | Location, ambient, lubricant, load and operating point | Thermal trend |
| Seal leakage | Rate/pattern, pressure, temperature, seal arrangement and photos | Seal/process/mechanical evidence |
| Flow and head | Flow, suction/discharge pressure, speed and valve condition | Hydraulic change |
| Motor load | Current/power, speed and operating condition | Load change |
| Maintenance history | Failure mode, date, parts and work scope | Repeat pattern |
Related guides: ANSI Pump Vibration Troubleshooting and Low-Cost Pump Condition Monitoring.
Pillar 4: Supply Quality and Traceability
“Interchangeable” should not mean only that the equipment appears to fit. Replacement review should separate five compatibility questions.
Evidence to Define Before Release
- Controlled drawing and revision.
- Material grade and traceability where required.
- Dimensional inspection and critical fits.
- Runout or rotating-component inspection where applicable.
- PMI, hydrostatic test, performance test or witness requirements where specified.
- Deviation/concession and final approval records.
Related guide: ANSI B73.1: Dimensional Interchangeability vs Real Compatibility.
A Practical Root-Cause Failure Review
Root-cause review does not need to begin with a complex model. It needs a disciplined sequence that keeps the symptom separate from the cause.
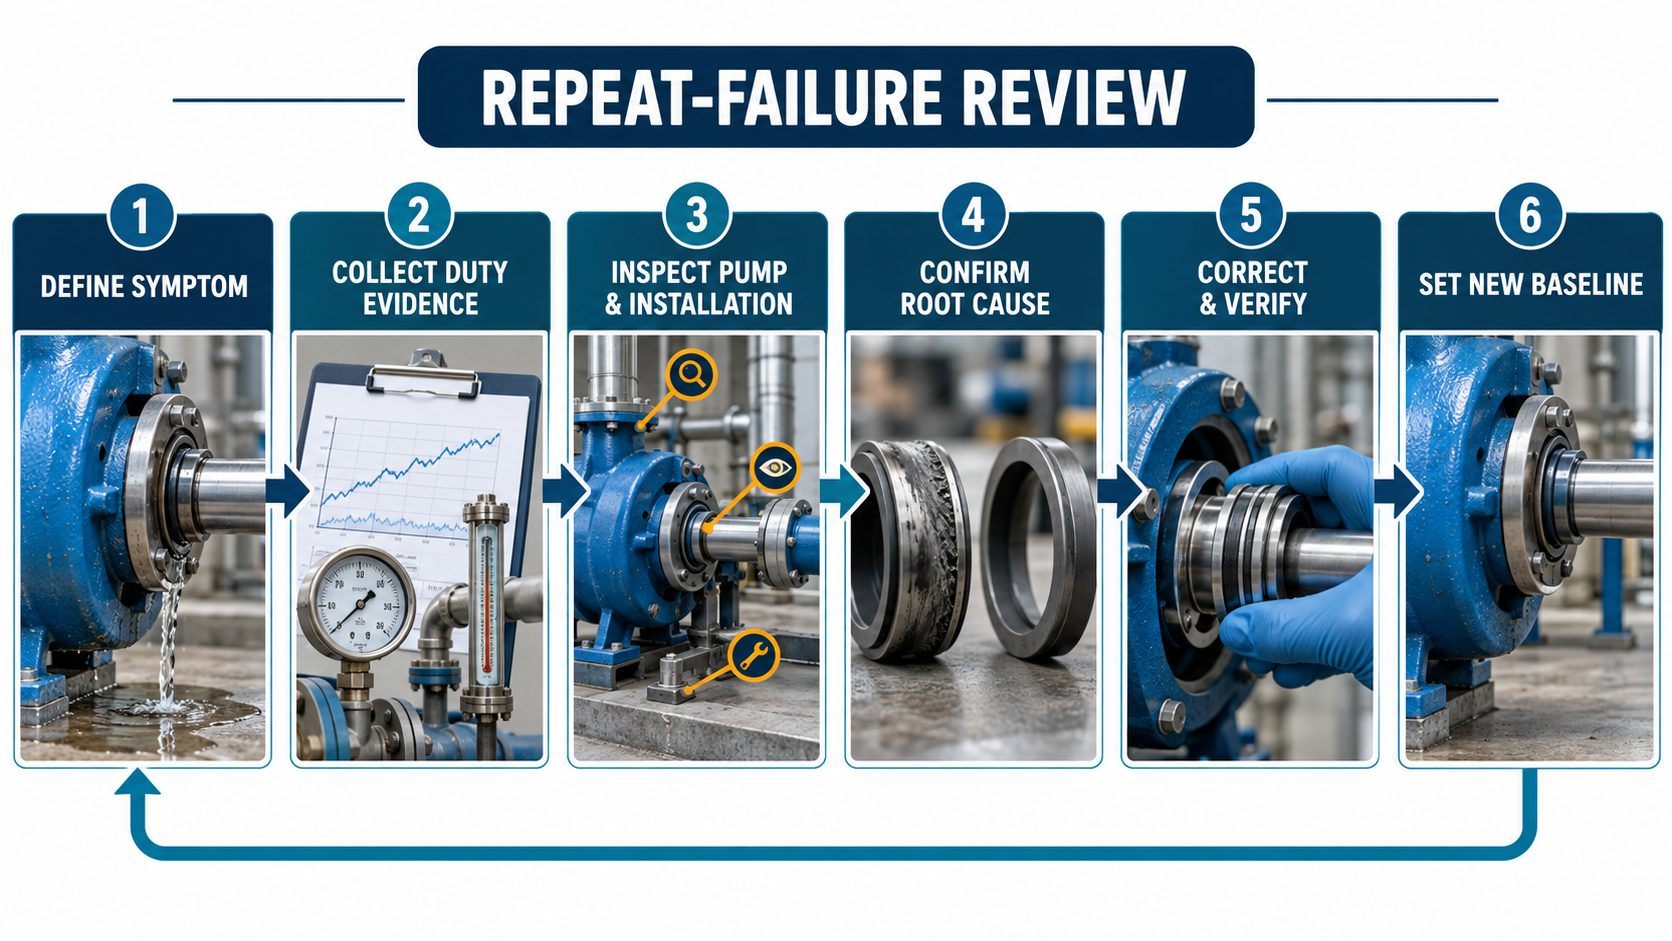
1. Define the symptom
Record the observable failure without calling it the cause.
2. Establish the operating state
Record flow, pressure, speed, liquid condition and controls at the time the symptom appears.
3. Check hydraulic evidence
Compare actual duty with the applicable curve, operating region, power and NPSH basis.
4. Check installation evidence
Review foundation, alignment, piping, supports and thermal movement.
5. Review condition trends
Compare vibration, temperature, leakage, load and hydraulic performance before failure.
6. Inspect the failed component
Use wear, pitting, rubbing, corrosion, deposits, heat or dimensional evidence to test the working hypothesis.
7–9. Correct, verify and establish a new baseline
Correct the mechanism supported by the evidence, repeat the relevant measurements and document the stable post-correction condition.
Worked Diagnostic Example: Repeat Mechanical-Seal Leakage
A process pump develops repeated mechanical-seal leakage. The seal is replaced and the pump returns to service, but leakage later returns. A second seal replacement without new evidence would repeat the same maintenance strategy.
Hydraulic Review
Confirm the operating point, suction condition, speed and whether the symptom correlates with a specific duty state.
Installation Review
Check alignment, piping influence, shaft/runout evidence and mechanical condition.
Condition Evidence
Compare vibration, temperature and leakage trend before the failure.
Supply / Configuration Review
Confirm the correct pump and seal interfaces, configuration and relevant inspection evidence.
Decision and Verification
Select the corrective action only after evidence supports a mechanism, then verify the same measurements after correction.
Repair the Pump, Correct the System, or Replace It?
- Duty remains suitable.
- Major interfaces remain serviceable.
- Failure mechanism is understood.
- Controlled repair restores required condition.
- Operating point is unsuitable.
- Suction or piping condition is responsible.
- Controls repeatedly drive off-design operation.
- Process conditions changed.
- Duty materially changed.
- Current pump cannot meet the required envelope.
- Major condition makes repair unattractive.
- Service/material requirement changed.
ANSI Pump Reliability Field Checklist
Before another repair, collect as many of these items as practical.
- Model and size
- Speed
- Impeller configuration
- Driver information
- Flow
- Suction/discharge pressure
- Liquid and temperature
- Control state
- Alignment
- Soft foot
- Coupling
- Pipe supports
- Runout where relevant
- Vibration
- Bearing temperature
- Seal leakage
- Motor load
- Performance trend
- Failure date
- Photos
- Inspection findings
- Previous corrective action
- GA / drawing
- Material
- Critical dimensions
- Required test / inspection scope
Technical References
ANSI/HI 9.6.1 — NPSH Margin
ANSI/HI 9.6.2 — Allowable Nozzle Loads
ANSI/HI 9.6.3 — Operating Regions
ANSI/HI 9.6.4 — Vibration Measurements and Allowable Values
ANSI/HI 9.6.5 — Condition Monitoring
ANSI/HI 9.6.6 — Pump Piping
ITT Goulds 3196 i-FRAME IOM — OEM-specific installation/alignment example
Use the latest applicable edition required by the project. References do not replace the selected pump manufacturer’s current documentation, approved drawings or purchase specification.
Frequently Asked Questions
What are the four pillars of ANSI pump reliability?
Hydraulic duty, installation and alignment, condition evidence, and supply quality with appropriate dimensional, material and inspection documentation.
Does a failed bearing identify the root cause?
No. Bearing damage can be associated with lubrication, contamination, installation, alignment, hydraulic load, electrical current, temperature, fit or another rotating-machine condition.
Why does a mechanical seal fail repeatedly?
Repeated seal leakage can involve the seal itself, but it can also be associated with hydraulic operation, suction conditions, shaft movement, runout, alignment, piping influence or the seal-support system.
Should every ANSI pump operate between 70% and 120% of BEP?
No universal percentage should be assumed for every pump. Use the manufacturer’s documented operating region and applicable project criteria.
Is there one universal NPSH margin for ANSI process pumps?
No. NPSHa is determined by the system, NPSHr comes from the selected pump and flow, and the required margin depends on the application and applicable guidance.
What vibration level is acceptable for an ANSI pump?
Use the applicable OEM requirement, project specification and relevant pump vibration standard, interpreted with measurement location, direction, speed, load and hydraulic condition.
How can pipe strain affect pump reliability?
Piping loads can act on the casing/nozzles and may influence machine position or alignment. Review flange fit, supports, before/after alignment and applicable nozzle-load requirements.
What information is useful for a reliability review?
Start with pump model/size, operating flow/head, speed, liquid/temperature, failure description, photos, maintenance history and any available vibration, temperature, alignment or piping evidence.

